Outlook: Automation in High-Volume Closed-Die Forging
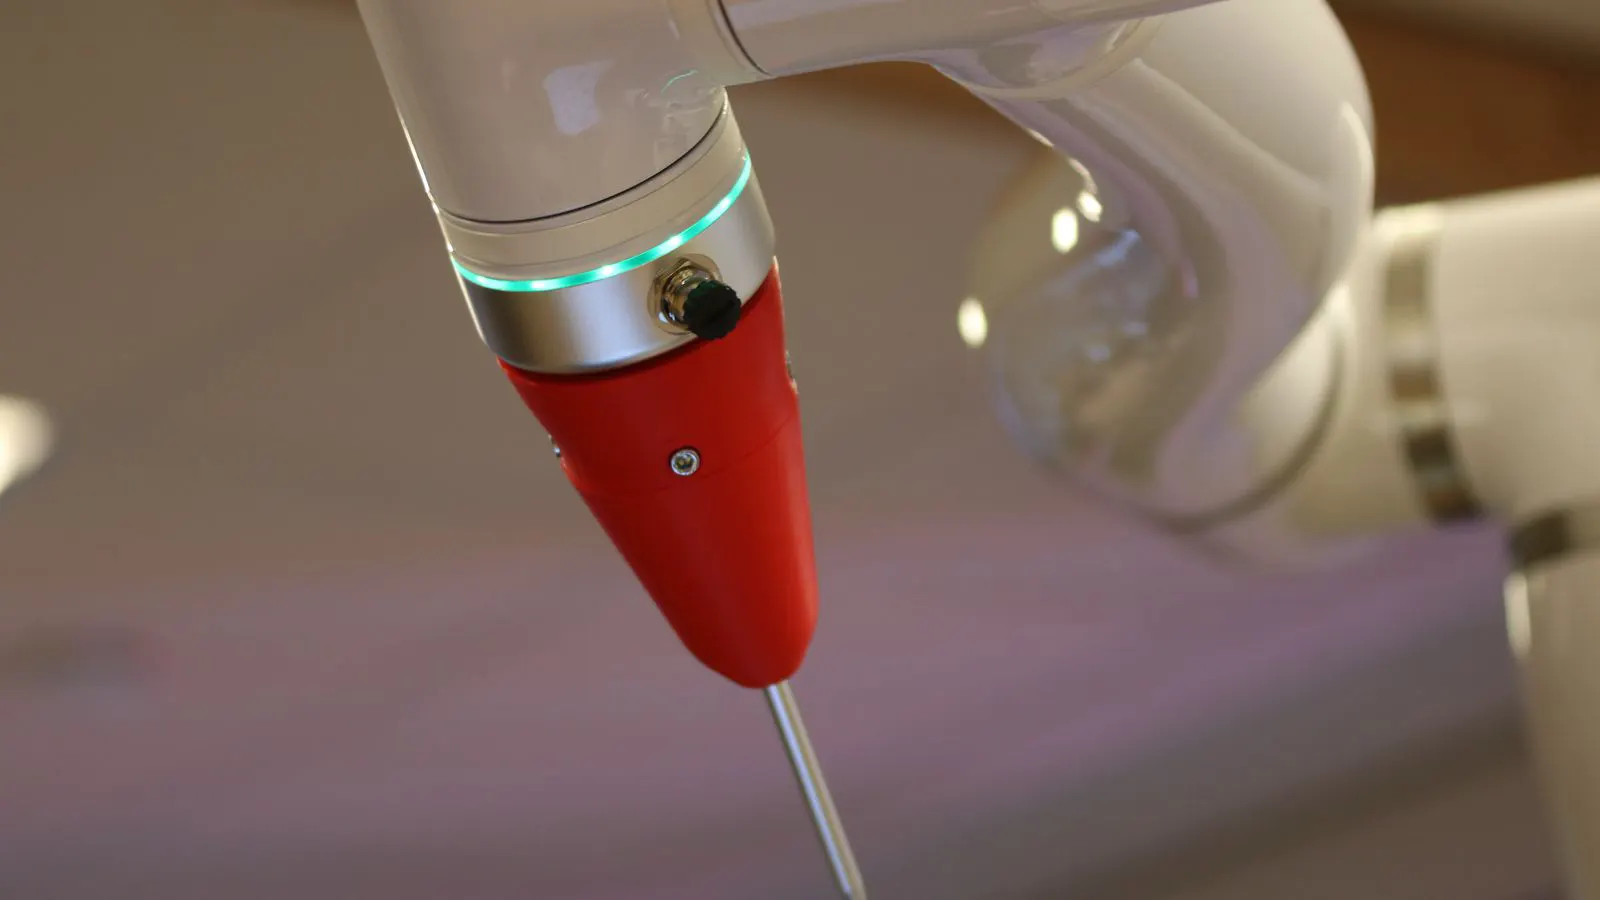
High-volume closed-die forging is shifting from manual labor to integrated robotics. This outlook outlines five key shifts in economics and operations, focusing on how automation affects cost, cycle time, and workforce planning.
- Automation in closed-die forging focuses on material handling, die changeovers, and quality inspection rather than just pressing.
- The economic model shifts from labor cost to capital investment and maintenance.
- Workforce roles change from manual operators to process monitors and robotic programmers.
- Integration with existing production lines is more complex than installing a single new machine.
- Buyers should prioritize flexible automation systems that can handle multiple die sets.
The Changing Economics of High-Volume Forging
High-volume closed-die forging has traditionally relied on a balance between press capacity and manual labor. Operators load the die, remove the hot forging, and manage the flash. This model works for moderate volumes but faces pressure as cycle times drop and production targets rise. Automation changes the cost structure. The variable labor cost per part decreases, but the fixed cost of the system increases. For manufacturers running long shifts with multiple die sets, the shift from manual handling to robotic handling alters the break-even point for high-volume runs.
The core question for buyers is no longer “can the press run faster?” but “can the line handle the parts without human intervention?” The answer depends on how well the automation integrates with the existing infrastructure.
Where Forging Automation Actually Fits
Robotic automation in closed-die forging does not replace the press. The press performs the deformation. Robots handle the material movement around the press. This distinction is critical for cost planning.
- Material Loading: Robots pick blanks from a magazine or conveyor and place them into the die. This removes the need for a human to stand in the press area during the cycle.
- Part Removal: After the press cycle, the robot extracts the hot forging from the die and places it on a cooling conveyor or directly to the next operation.
- Die Changeover: This is the most valuable application. Changing a die set manually can take hours. A robotic system can assist in die alignment and positioning, reducing downtime between different part families.
- Quality Inspection: Robots can move parts to vision systems or dimensional check stations immediately after the forging cycle. This allows for real-time rejection of defective parts before they move to machining.
A single robotic cell can serve multiple functions. The same arm used to load the die can also remove the part and place it on a cooling table. This multi-functionality reduces the number of machines required and simplifies the line layout.
Shift One: From Labor Cost to Capital Cost
The primary economic shift is the movement of cost from variable labor to fixed capital. In a manual operation, the labor cost per part is relatively stable. If the press runs faster, you can still use the same number of operators up to a limit. When that limit is reached, you must add more operators or reduce cycle times.
With forging automation, the labor cost per part drops significantly. One operator can monitor multiple robotic cells. However, the initial investment is high. You are buying industrial robots, programmable logic controllers, sensors, and safety systems. You are also buying integration time. The cost of programming the robot to handle the specific geometry of the die and the blank is a fixed cost that must be amortized over the production life of the part family.
This shift favors high-volume, stable part families. If you are running a die set for only a few weeks, the capital cost of automation may not pay off. If you are running a die set for years, the labor savings and the ability to run the line unattended for extended periods justify the investment. The planning horizon for automation must be longer than the planning horizon for manual labor.
Shift Two: Cycle Time and Throughput
Automation allows for tighter integration of the material handling process with the press cycle. In a manual setup, there is a gap between the press completing its stroke and the operator loading the next blank. This gap is often called the “dead time.” The press is ready, but the next material is not in position.
Robotic systems can be programmed to prepare the next blank while the current cycle is finishing. This is called overlapping operations. The robot moves the finished part to the cooling conveyor and simultaneously positions the next blank in the die. This reduces the dead time to the minimum required for the robot to move. The result is a higher parts-per-hour rate without increasing the press cycle time itself.
This shift in throughput has a direct impact on capacity. A press with a ten-second cycle time and manual loading might produce 500 parts per hour. The same press with a robotic loading system that eliminates half the dead time might produce 650 parts per hour. The difference is not in the press, but in the flow of material. For buyers, this means that automation can extend the life of existing press equipment. Instead of buying a larger press to meet demand, you can buy a robotic cell to make the existing press work harder.
Shift Three: Workforce and Skill Requirements
The workforce in a forging shop changes when automation is introduced. The manual operators who once spent their time walking to the press, picking up hot parts, and clearing flash are no longer needed in the same numbers. Their roles evolve.
- Programming: Technicians must learn to program the robots. This involves understanding the robot’s coordinate system, the safety zones, and the logic for material handling.
- Maintenance: Robots have complex mechanical and electrical systems. They require regular calibration, lubrication, and sensor checks. The maintenance team needs new skills to keep the robotic cells running.
- Process Monitoring: Instead of watching the press, operators watch the data. They monitor the robot’s performance, the quality of the parts, and the flow of material. They step in only when an alarm is triggered.
This shift in skills requires a training plan. You cannot simply replace manual operators with programmers. You must build a team that understands both the forging process and the automation technology. The transition period can be difficult. The workforce may resist the change, and the new system may not run at full capacity until the team is comfortable with it. Planning for this training period is as important as planning for the equipment purchase.
Shift Four: Flexibility and Die Changeover
High-volume forging often involves running multiple die sets on the same press. Each die set is designed for a specific part. Switching from one die set to another is a major event. It requires removing the old die, cleaning the press, and installing the new die. This process is time-consuming and often requires manual labor.
Robotic automation can assist in this process. Some systems are designed to help with die alignment. The robot can position the die in the press and verify its location before the cycle begins. This reduces the time needed for setup. More advanced systems can store multiple die sets in a rack and bring the next one to the press when needed. This is called die automation. It allows the press to run continuously with different part families, with minimal downtime.
This flexibility is valuable for manufacturers that produce a variety of parts. It reduces the need for multiple presses. A single press with a die automation system can run a high mix of parts. This is particularly useful in the automotive industry, where part families change frequently. The ability to switch dies quickly means that the press can be used for more part families, increasing its utility and reducing the total number of presses needed.
Shift Five: Quality and Traceability
Automation in closed-die forging changes the quality control process. In a manual setup, quality checks are often done at the end of the line. Parts are moved to a inspection station, where they are measured. If a part is out of tolerance, it is rejected. But by then, it has already gone through several processes.
With robotic automation, quality checks can be integrated into the line. The robot can move the part directly to a vision system or a dimensional check station. The system measures the part immediately after the forging cycle. If the part is defective, the robot can remove it from the line before it moves to the next operation. This reduces waste. You do not spend time machining a part that will be rejected anyway.
Traceability is also improved. Each part can be identified by a unique code or by its position in the batch. The robotic system can log the data for each part. This means that if a defect is found later in the production process, you can trace it back to the specific die cycle and the specific robot movement. This is valuable for quality audits and for identifying root causes of defects.
How to Prepare for Forging Automation
Preparing for the introduction of forging automation requires a careful assessment of your current production environment. You need to understand your part families, your press capacity, and your workforce skills.
- Audit Your Part Families: Identify which part families run at the highest volumes and which have the longest production runs. These are the best candidates for automation. Parts that run for short periods may not justify the capital investment.
- Evaluate Your Press Infrastructure: Check the condition of your presses. Automated cells require reliable press controls. If your presses are old, you may need to upgrade the controls before adding robots.
- Assess Your Workforce: Identify which employees have the skills to program and maintain robotic systems. If you do not have these skills, plan for training. You may need to hire new technicians or send current employees to training programs.
- Plan for Integration: Automation is not a standalone system. It must integrate with your existing material handling, quality control, and production management systems. Plan for the interfaces between the robotic cells and the rest of your shop floor.
- Start with a Pilot: Consider starting with a single robotic cell for one die set. This allows you to test the system and train your team before committing to a full line automation. A pilot project can reveal issues with the integration and help you refine your approach.
The Road Ahead
The future of high-volume closed-die forging is moving toward greater integration. Forging automation is not just about replacing manual labor. It is about creating a more efficient, flexible, and high-quality production system. The shifts in economics, throughput, workforce, flexibility, and quality are interconnected. They all point to a production model where the robot is the primary interface between the press and the material.
Buyers who plan for these shifts will be better positioned to manage the transition. The key is to view automation as a system, not just a machine. The value comes from the integration of the robot with the press, the die, the material, and the workforce. When these elements work together, the production efficiency improves, and the economics of high-volume forging change in favor of the manufacturer.
| Component | Role in Automation | Impact on Economics |
|---|---|---|
| Industrial Robot | Handles material, assists die changeover | Reduces labor cost, increases throughput |
| Press Controls | Coordinates press cycle with robot | Enables overlapping operations, reduces dead time |
| Quality System | Inspects parts immediately after forging | Reduces waste, improves traceability |
| Workforce | Programs, maintains, monitors the system | Requires new skills, changes labor mix |
| Die Automation | Stores and positions multiple die sets | Increases flexibility, reduces downtime |
| Material Magazine | Stores blanks for the robot to load | Ensures continuous supply, reduces manual handling |
Frequently asked questions
Can forging automation be applied to low-volume part families?
Generally, no. The high capital cost of robotic systems and integration makes them less suitable for short production runs. Low-volume parts are better suited to manual handling or semi-automated systems.
What is the main difference between manual and robotic material handling?
Robotic handling allows for overlapping operations, where the next blank is prepared while the current cycle finishes. This reduces dead time and increases throughput without changing the press cycle time.
How does automation affect the workforce in a forging shop?
The role of the operator shifts from manual handling to monitoring and programming. Operators must learn to program robots, maintain the systems, and monitor production data.
Is die automation a common feature in high-volume forging?
It is becoming more common. Die automation allows a single press to run multiple part families with minimal downtime. It is particularly useful for manufacturers with high part mix requirements.
What is the first step to preparing for forging automation?
Audit your part families to identify which ones run at the highest volumes and have the longest production runs. These are the best candidates for automation.


